Flex-hone® Flexible Honing Tools

Features | Product Range | How To Select | How To Use
Flex-hone® Ball Hone Flexible Honing Tool
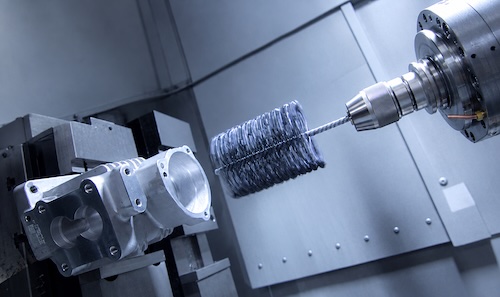
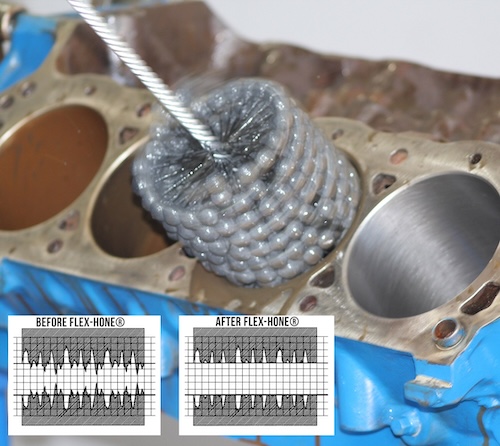
The Flex-Hone® Tool produces a controlled surface condition unobtainable by any other method.
It involves finish, geometry and metallurgical structure.
A high percentage plateau free of cut, torn and folded metal is produced.
The Flex-Hone® is a resilient, flexible honing tool with a soft cutting action.
The abrasive globules each have independent suspension that assures the Flex-Hone® to be self-centering, self-aligning to the bore, and self-compensating for wear.
Flex-Hones® are sometimes called or referred to as Ball Hones, Dingleberry Hones, dingleberry hone, grape hone, bead hone, bottle brush hone, glaze buster/breaker hone, or flexible hone
The Flex-hone® Tool produces a controlled surface finish unobtainable by any other method. A high percentage plateau surface is produced free of cut, torn and folded metal.
Features
- Simple and easy to use, powered by an ordinary drill
- Available for bores from 5/32 to 36, 4mm to 914mm diameter
- Creates a high percentage plateau surface
- Deburrs cross holes
- Edge blends
- Self-centering
- Self-aligning to bore
- Self-compensating for wear.
If Your Specifications Call For:
- A plateaued finish over 50%
- A finish free from cut, torn and folded metal and...
If You Want:
- Lowered oil consumption
- Less blow-by
- Less Friction...
FLEX-HONE® TOOLS Product Line

Flex-Hone® for Rotors
Disc rotor finishing tool.

Miniature Flex-Hone®
4mm (.157"), 4.5mm (.177"), 4.75mm (3/16")

Brake Cylinder, Hydraulic, Valve Guide Flex-Hone®
Sizes from (.197") to 3", 5mm to 76mm

Disc Brake Flex-Hone®
Sizes from 1 ½" to 3 1/8" , 38mm to 79mm

Block Cylinder or Liner Flex-Hone®
Sizes from 3" to 8" , 76mm to 203mm

Heavy Duty Flex-Hone®
Sizes from 8 ½" to 36", 203mm to 914mm , shafts sold separately.


Specialty Flex-Hone® Tools
Shotgun, Paintball Gun, Handgun

Diamond Flex-Hone® Tools
for finishing carbide, ceramic and hardened tool steel

Flex-Hone® Accessories
Flex-Hone Oil, Cylinder Washing Brush, Pipe Nipple Adaptors, Flex-Shaft
How to Select
1) Size
2) Abrasive Material
3) Grit
STEP 1 - TOOL DIAMETER SELECTION
STEP 2 - ABRASIVE TYPE SELECTION
Abrasive type is determined by the material you are working with. Refer to the chart for guidance.
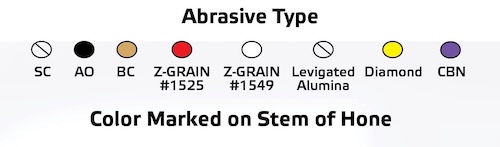
| IF THE BASE MATERIAL IS: | SUGGESTED ABRASIVE MATERIAL |
| Mild steel, stainless steel and cast iron | Silicon Carbide (SC) |
| Aluminum, brass, bronze and softer metals. For deglazing Nikisil cylinders, we suggest 240 AO | Aluminum Oxide (AO) |
| Low carbon to medium carbon steels, stainless steel and cast iron. | Zirconia Alumina (Z-Grain). Z-Grain is also beneficial when you are looking for longer tool life than SC |
| Medium to high carbon steels and heat-treated steels to 50 Rc. It is also useful in titanium. | Boron Carbide (BC) |
| For a final polish on many materials | Levigated Alumina |
| For carbide, ceramic, hardened tool steel | Diamond |
STEP 3 - GRIT SELECTION
The amount of work to be performed and the degree of surface finish improvement required govern grit selection. Coarse finishes may require progressively finer FLEX-HONE® tools to meet final surface finish requirements. In very general terms, final finish will be in the following ranges. This chart is intended to offer a starting point in selecting a grit but the final selection must be verified by actual trial.
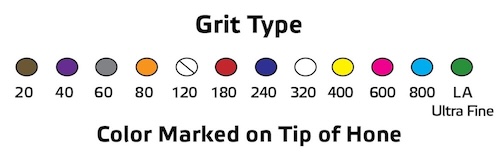
| Grit | Finish Range |
|---|---|
| 800-LA (2500 MESH) | Ra 3-10 (.05 – .2 Micrometer) |
| 600 | Ra 8-12 (.2 – .3 Micrometer) |
| 400 (800 MESH) | Ra 10-20 (.3 – .6 Micrometer) |
| 320 | Ra 18-30 (.5 – .7 Micrometer) |
| 240 | Ra 24-32 (.6 – .8 Micrometer) |
| 180 (170/200 MESH) | Ra 30-40 (.7 – 1.0 Micrometer) |
| 120 | Ra 35-50 (.9 –1.4 Micrometer) |
| 80 | Ra 45-64 (1.2 – 1.6 Micrometer) |
| 60 | Ra 60-80 (1.5 – 2 Micrometer) |
| 40 | Ra 70-125 (1.7 – 3.2 Micrometer) |
| 20 | Ra 125-250 (3.2 – 6.3 Micrometer) |
How to Use
The flex-hone tool should be securely held in a collet chuck or similar holding device.
It is best to use the shortest shank possible for your application.
The tool can be chucked in a standard 3/8 inch or 1/2 inch drill motor, drill press, milling machine, lathe machine tool collet or any rotating spindle.
The flex hone tool always requires the use of a lubricant or honing oil
RPM and Stroke rate
The Flex-Hone tool is a low RPM tool. Specific RPM is dependent on the diameter of the tool and the application. General speed ranges are given but, again, machine trials are required to verify the parameters.
Hone Dia. RPM
19" to 36" 60-120 RPM
12" to 18" 80 to 350 RPM
8" to 12" 300 to 500 RPM
4" to 8" 400 to 600 RPM
2" to 4" 600 to 800 RPM
½" to 2" 700 to 900 RPM
4mm to ½" 800-1200 RPM
Stroke rate is a function of Flex-Hone diameter, stroke length and cross hatch angle specification, if any. High crosshatch angles require faster stroke rates. The larger diameter tools might feed as slow as 10-12 IPM while the smaller diameter tools with high cross hatch angles might require feed as high as 250 IPM.
The hone can be made to rotate in both directions. Often this is preferable to do on each work piece (i.e. 5 strokes clockwise, 5 strokes counterclockwise)
General Application and Selection of the Flex-Hone® Tool, flexible honing tools
Flex-Hone® Tools in Canada
Newman Tools is a Canadian supplier of Brush Research Flex-Hone® flexible honing tools. Based in Ottawa, Ontario, we supply Flex-Hone tools across Canada and worldwide. Our selection includes miniature, brake-cylinder, hydraulic, valve-guide, block-cylinder, heavy-duty, rotor, disc-brake and specialty Flex-Hone tools.
Sept 2026 , May 2022, September 2020, May 2019, October 2018,June 2016,Sept 2013, July 2010, September 2009, June 2009, April 2009, Aug 2007 March 2006
The descriptions, illustrations, specifications, dimensions, and part numbers are subject to change without notice.